GN Separation has recently supplied its self‑developed Stack Vibrating Screen to a domestic mining enterprise, delivering a tailored fine‑grained screening solution for mineral processing operations. By merging the compact multi‑layer strengths of stacked screening equipment with high‑frequency fine‑screen separation performance, this unit targets fine‑particle classification, wet screening and dewatering challenges across mining workflows.
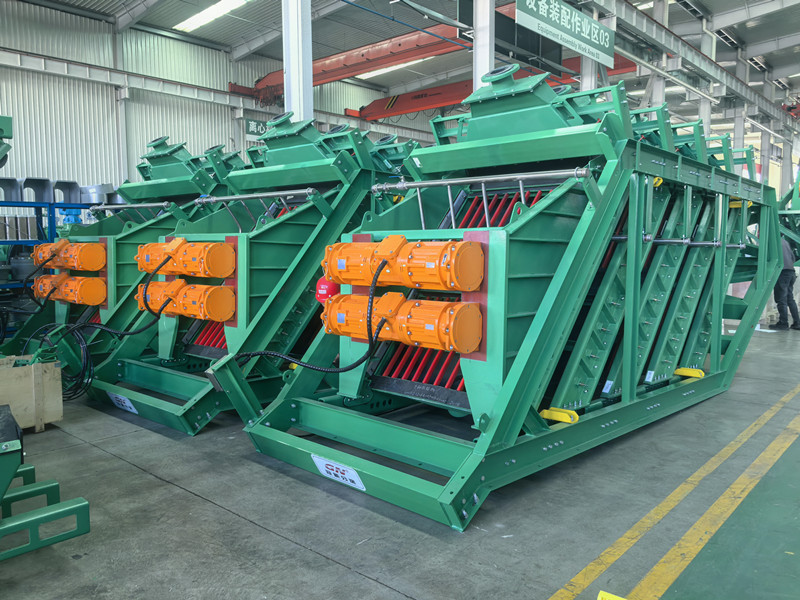
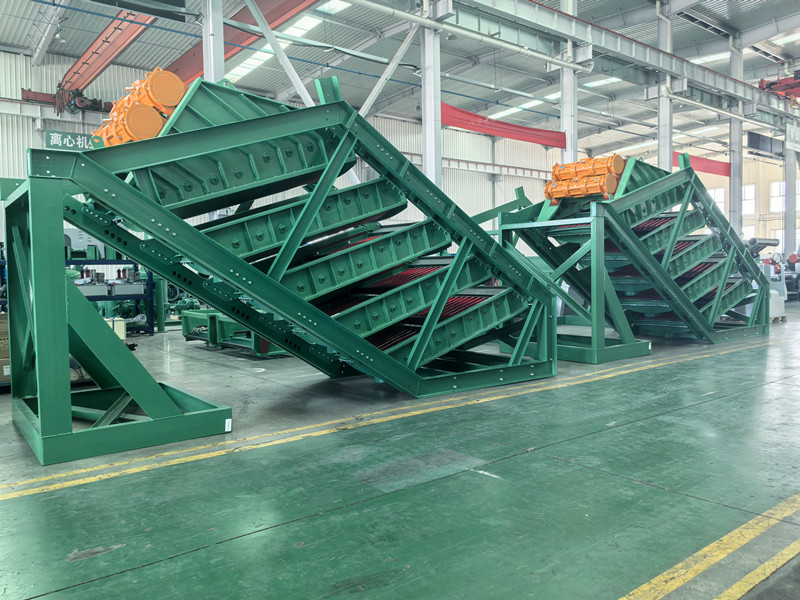
Conventional vibrating screens mostly rely on a single screening surface, which often calls for multiple separate machines to achieve required throughput for fine‑material handling. GN’s stack vibrating screen adopts a flexible multi‑deck architecture, configurable from 2 to 5 screening layers according to site layout and actual process requirements. Multiple screening surfaces operate within one compact frame, drastically cutting footprint occupancy while retaining adjustable processing capacity. This makes it well‑suited for mineral processing, coal preparation and other sectors demanding reliable fine‑particle separation.
At the heart of this equipment lies GN’s in‑house engineered vibration system built upon the two‑degree‑of‑freedom resonance principle. Driven as a single vibration source by twin imported vibration motors, the entire screen assembly produces stable linear vibration. The high‑frequency motion satisfies rigorous fine‑particle screening needs and facilitates efficient solid‑liquid separation during wet screening and dewatering cycles.
Combining high‑frequency excitation with stacked multi‑deck structures, the GN Stack Vibrating Screen brings together the core merits of stack screening and fine‑screen technology. It addresses two common pain points for mineral processors: pursuit of high screening efficiency and limited available installation space.
Mining sites vary greatly in feedstock properties, incoming material conditions and production targets. That is why the stack vibrating screen supports flexible 2‑to‑5‑layer configurations, enabling operators to match equipment set‑up to their classification and separation objectives.
Precise fine‑particle screening carries substantial weight in mineral processing flowsheets. Accurate classification optimizes downstream beneficiation performance; thorough dewatering lowers residual moisture of final products and simplifies subsequent stockpiling, handling and transportation.
As a seasoned manufacturer focused on solid‑liquid separation and screening solutions, GN Separation keeps iterating its product portfolio to meet evolving mining‑industry demands. The high‑frequency stack vibrating screen embodies GN’s commitment to merging field‑proven mechanical design with proprietary technology development.
This recent delivery to a local mining firm further validates GN Separation’s expertise in fine‑material screening and mineral‑processing applications. Moving forward, GN will keep supplying robust screening hardware and custom‑engineered solutions aligned with each customer’s process parameters.
If you would like to learn more about GN’s stack vibrating screen or other mineral‑processing separation equipment, feel free to get in touch with our team.
- Details
-
Published: 15 November 2026
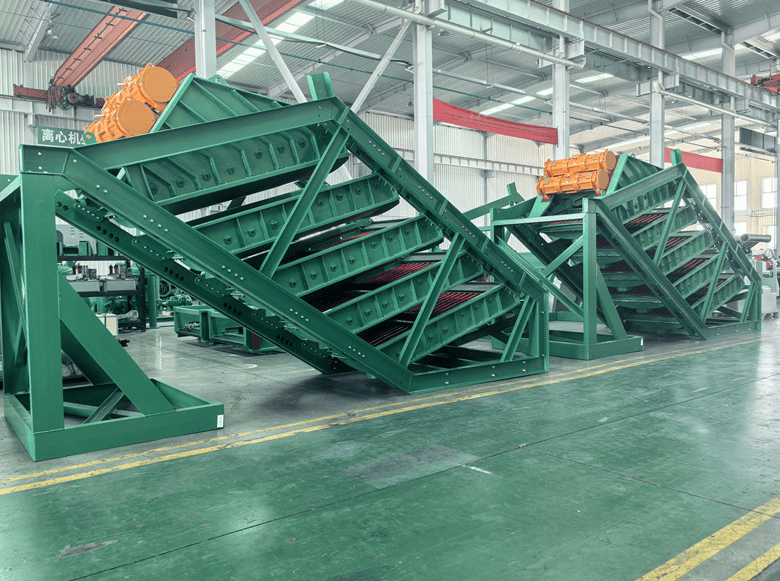
GN Separation has developed its high-frequency stack vibrating screen technology to provide efficient fine particle screening and classification solutions for the mining industry. Recently, GN introduced its Stack Vibrating Screen to a domestic mining company, offering a solution designed to improve screening efficiency, optimise processing capacity and reduce equipment footprint.
- Details
-
Published: 13 November 2026
GN Separation delivered a custom‑engineered decanter centrifuge solution for a canola oil clarification project in Australia. Tailored to edible‑oil processing workflows, the unit prioritizes high‑efficiency solid‑liquid separation alongside strict hygiene standards, operational versatility and long‑term operational dependability.
To satisfy the unique demands of edible‑oil production, GN optimized the centrifuge’s internal construction for this Australian end‑user. A core custom modification involves polishing the interior screw conveyor. Fine surface polishing delivers an ultra‑smooth screw surface, lowering material sticking and mitigating build‑up of residual process media within the machine. This feature carries critical importance for food‑grade processing: leftover residues could degrade over time and compromise product sanitary quality. The refined surface also simplifies in‑place cleaning and sustains a hygienic processing environment.
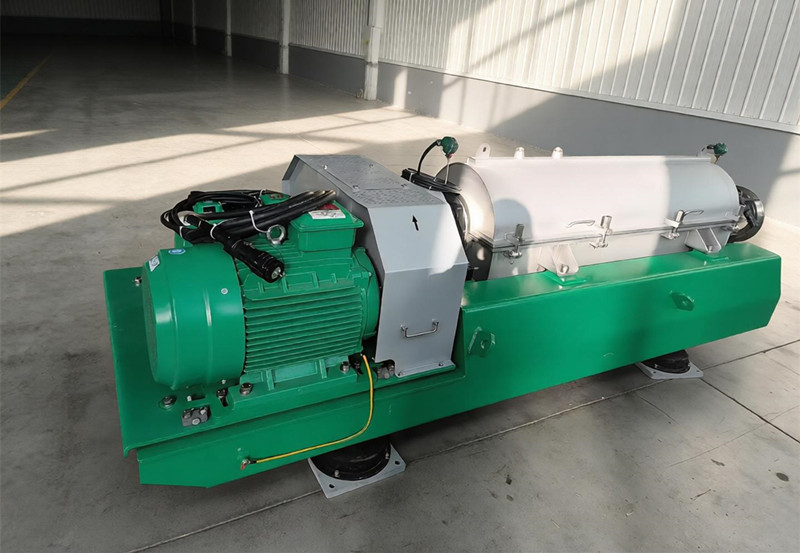
The system is also fitted with a centripetal pump for clarified liquid discharge. Traditional setups frequently require a full shutdown to modify liquid discharge parameters; by contrast, this pump enables operators to adjust the liquid pool depth on‑the‑fly, without halting centrifuge operation. Adjusting the pool depth allows operators to fine‑tune separation performance in response to real‑world feed properties and production targets. Such agility proves highly beneficial when handling feedstock with fluctuating solid loads or shifting process parameters. Unplanned downtime is cut down accordingly, enabling uninterrupted production and boosting overall process efficiency.
Beyond these custom design tweaks, the decanter centrifuge is built for steady, round‑the‑clock operation and consistent separation results. Boasting a compact footprint, continuous solid‑phase discharge and tunable operational parameters, it integrates seamlessly into full‑scale edible‑oil production lines. Equipment specifications are configured to match the client’s process goals, striking an optimal balance between separation efficacy, end‑product quality and ease of operation.
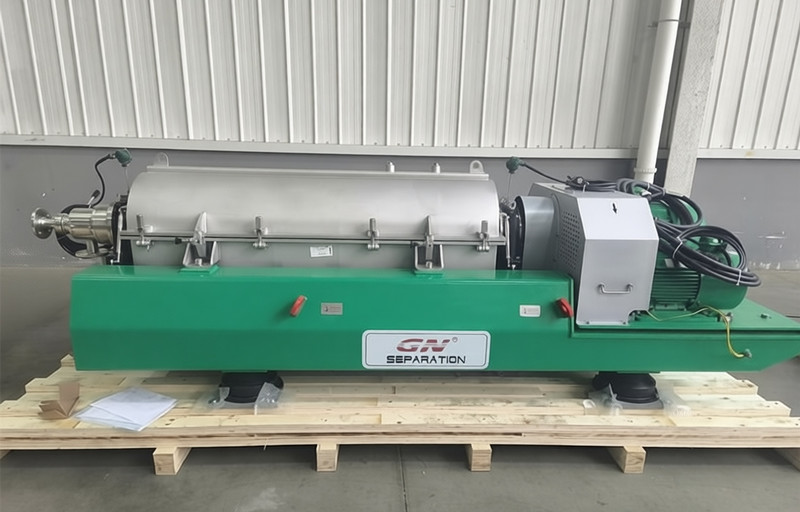
GN Separation possesses profound expertise in designing and fabricating industrial decanter centrifuges serving diverse sectors including food processing, wastewater treatment, oil‑gas and mineral processing. Since feed media and working conditions vary widely from project to project, GN adapts its separation technology to fit each project’s real‑world operational requirements.
This Australian canola‑oil clarification case exemplifies GN’s application‑oriented equipment philosophy. By pairing sanitary internal surface finishing with flexible liquid‑pool depth adjustment, GN supplies the client with a robust separation system that facilitates high‑throughput processing and stable product quality.
- Details
-
Published: 08 November 2026

Efficient Oil Clarification with Hygienic Design and Flexible Process Control
- Details
-
Published: 05 November 2026
GN Separation Reaches New Milestone: Five GNLW764-VFD Large-Bowl Decanter Centrifuges Up & Running at a High-Altitude Overseas Tailings Project
Decanter Centrifuge 1 We’re excited to share a major project win for GN Separation in the global mining industry: five of our GNLW764-VFD large-bowl decanter centrifuges have been successfully commissioned and are operating stably at an overseas mine tailings treatment site.
Built for tough slurry separation tasks, this installation is solid proof of GN’s ability to deliver custom solid-liquid separation solutions for some of the harshest mining environments on the planet.
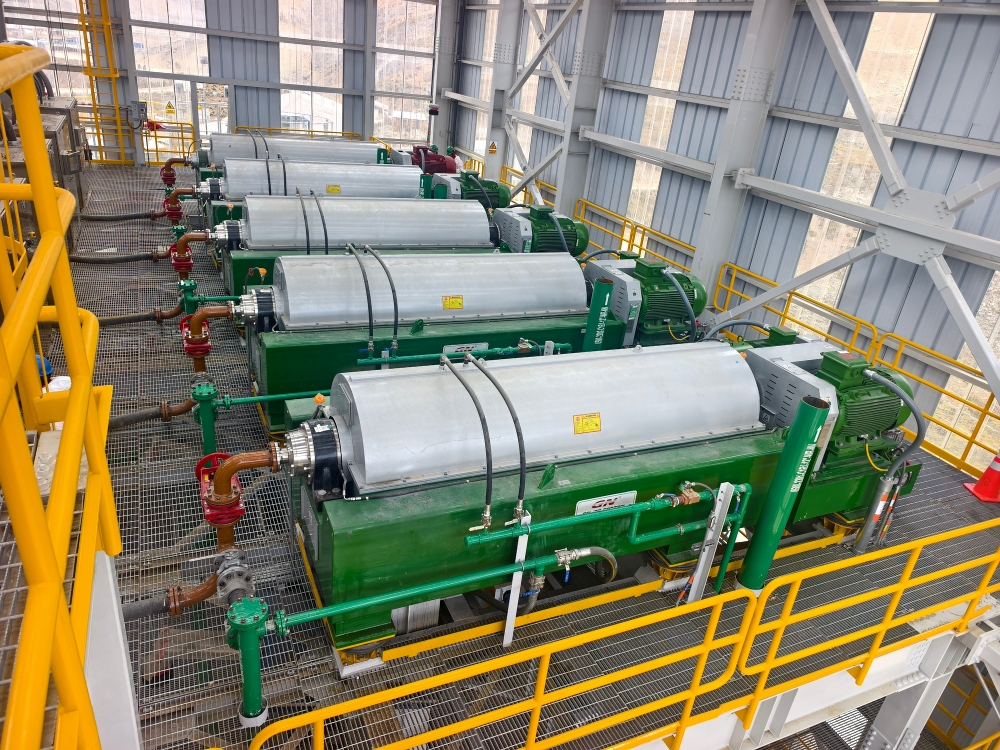
The project was awarded to GN after a competitive international procurement tender, serving a leading mining enterprise. From day one, the customer needed dependable equipment capable of handling massive volumes of tailings slurry under extreme working conditions.
The mine sits at an altitude of approximately 4,500 meters. This high-altitude location brought a unique set of obstacles: equipment performance, long-term operational stability and wear resistance were all put to the test.
On top of the extreme elevation, the tailings slurry features high flow rates and sharp, abrasive mineral particles that create heavy wear on a centrifuge’s core components. A standard, off-the-shelf centrifuge setup simply would not cut it. What the customer really needed was reliable long-run performance, efficient solid-liquid separation and manageable maintenance to keep their production targets on track.
To match these strict site conditions, GN developed a fully tailored equipment configuration. Our GNLW764-VFD decanter centrifuge comes with a 30-inch large-diameter bowl and variable-frequency drive (VFD) controls. The big bowl design supports high-capacity tailings processing, while variable-speed control lets operators adjust running parameters quickly to adapt to changing feed characteristics and separation demands.
Decanter Centrifuge 2 Wear resistance was one of our top design priorities for this project. Since abrasive slurry constantly erodes key components, we integrated specialized wear-resistant structures and carefully upgraded materials for all high-wear areas. These design choices boost equipment service life and make non-stop continuous operation feasible in this demanding mining setting.
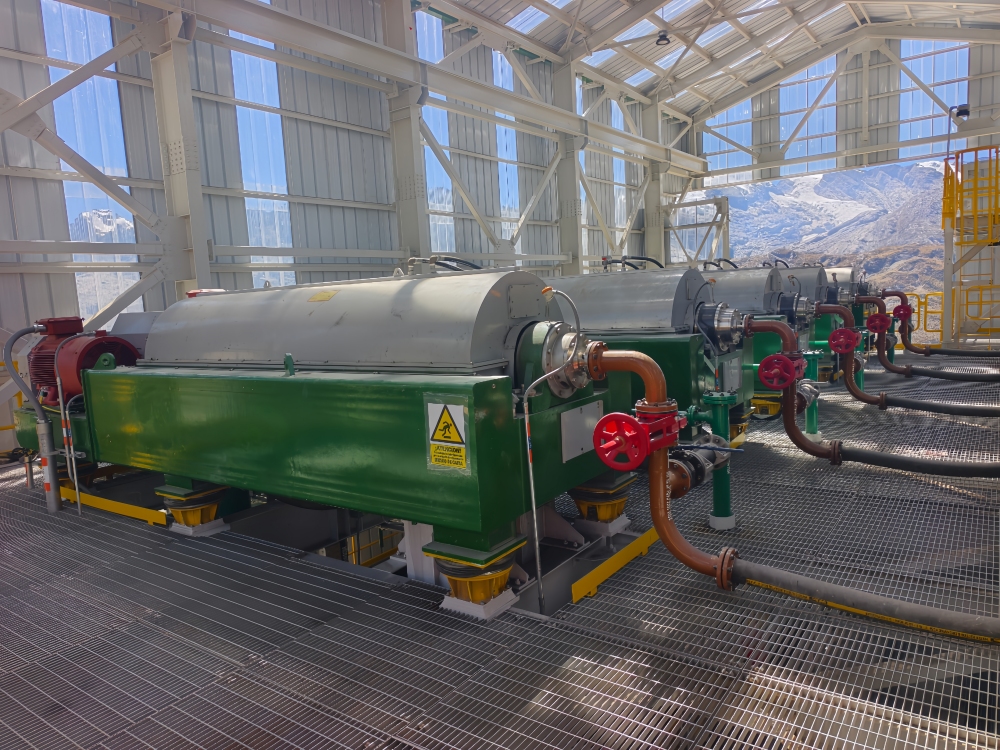
Rather than shipping all five centrifuges right away, we took a prudent, test-first approach. We delivered one unit first for full on-site trial. This test run allowed the customer to evaluate everything under real site conditions: separation results, running stability and whether the machine was fit for long-term production.
Once the field test was completed and performance fully verified, the customer was impressed with the results. They placed an additional order for four more identical centrifuges, expanding the project to a total of five GNLW764-VFD units. It’s a great example of how real-world trial testing builds confidence and lays the groundwork for larger system rollouts.
The full integrated tailings treatment package includes the five large-bowl decanter centrifuges, a 6,000-liter automatic chemical dosing unit and matched screw pumps. All equipment works as one unified system, supporting continuous feeding, flocculant conditioning and solid-liquid separation. This coordinated layout also simplifies daily operation and makes overall plant management much easier.
Decanter Centrifuge 3 For mining teams, well-designed tailings treatment is about more than just processing waste. It helps raise overall process efficiency, manage solid residues properly, and supports sustainable water and waste stewardship. By separating solids from slurry, decanter centrifuges reduce the volume of material that requires further downstream handling. They also create opportunities to recover and reuse process water, depending on ore properties and the overall plant layout.
The successful startup of all five centrifuges highlights GN Separation’s core advantage: we listen to tough site requirements and respond with custom equipment design, dedicated engineering support and rigorous on-site validation. From a single trial centrifuge to a complete five-unit system, this project showcases our practical, results-focused way of delivering reliable separation solutions for challenging overseas mining operations.
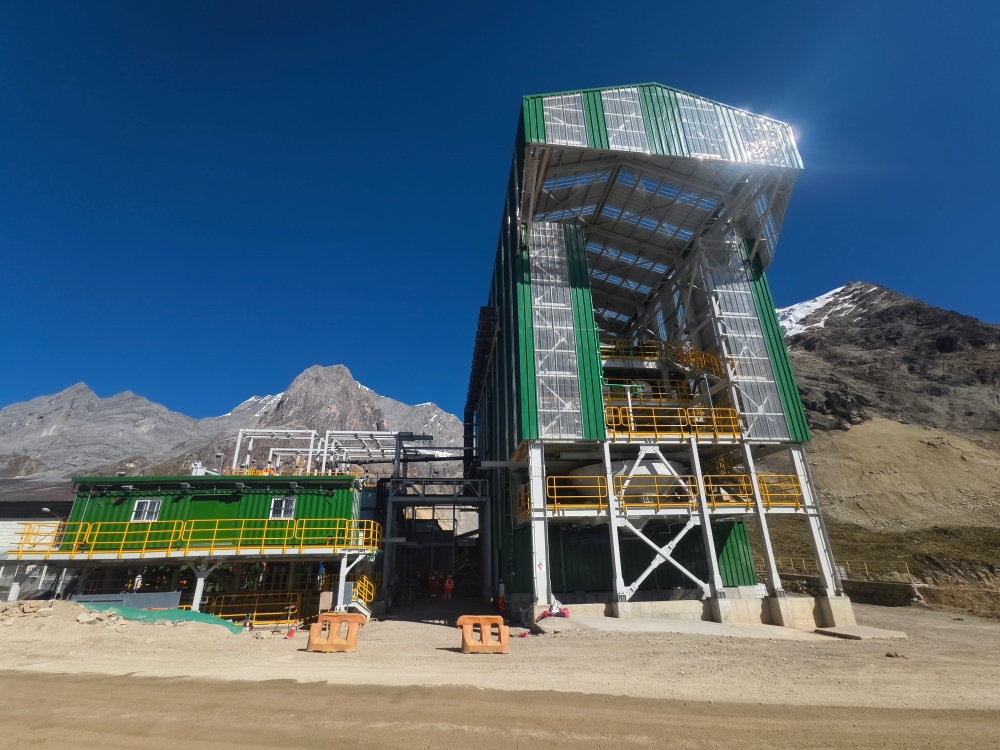
At GN Separation, we keep refining solid-liquid separation technologies for mining, mineral processing and industrial wastewater applications. By combining high-throughput decanter centrifuges with application-specific engineering and well-matched auxiliary equipment, our goal is to help mining clients around the globe boost treatment efficiency, maintain stable production and keep pace with evolving environmental standards.
- Details
-
Published: 01 November 2026
GN Separation is excited to announce that our GNLW764 Large-Bowl Decanter Centrifuge is ready for dispatch, destined for a mining tailings dewatering project. This heavy-duty decanter centrifuge stands as a strong testament to GN’s expertise in engineering robust solid-liquid separation equipment for harsh industrial working conditions.
Mining activities produce massive amounts of slurry laden with mineral fines, suspended solids and water. Effective solid-liquid separation is a cornerstone of mineral processing, wastewater handling and tailings management. As a continuous separation workhorse, the decanter centrifuge cuts slurry volume, streamlines solids handling workflows, and enables water recycling for reuse when site conditions allow.
The GN GNLW764 is purpose-built for high-throughput solid-liquid separation duties. Thanks to its large-diameter bowl, the unit achieves efficient centrifugal separation at high rotating speeds. In operation, denser solid particles settle onto the bowl wall. An internal screw conveyor transports these settled solids to the solids discharge port, while clarified liquid flows out via the liquid outlet. This fully continuous separation cycle delivers steady, consistent performance and minimizes manual maintenance requirements.
Mining slurry is typically highly abrasive with high solid content, placing heavy demands on processing equipment. Careful selection of equipment configurations and wear-resistant materials is critical to dependable long-term operation and extended service life. GN Separation customizes decanter centrifuge solutions tailored to diverse feed slurries and process objectives. We fine-tune every setup based on slurry properties, separation goals and on-site operational parameters.
Prior to shipment, the GNLW764 has passed a full suite of production verifications and stringent quality audits to meet the project’s technical specifications. From component assembly through final testing and pre-delivery preparation, we adhere to standardized manufacturing and quality control protocols to guarantee reliable equipment delivery.
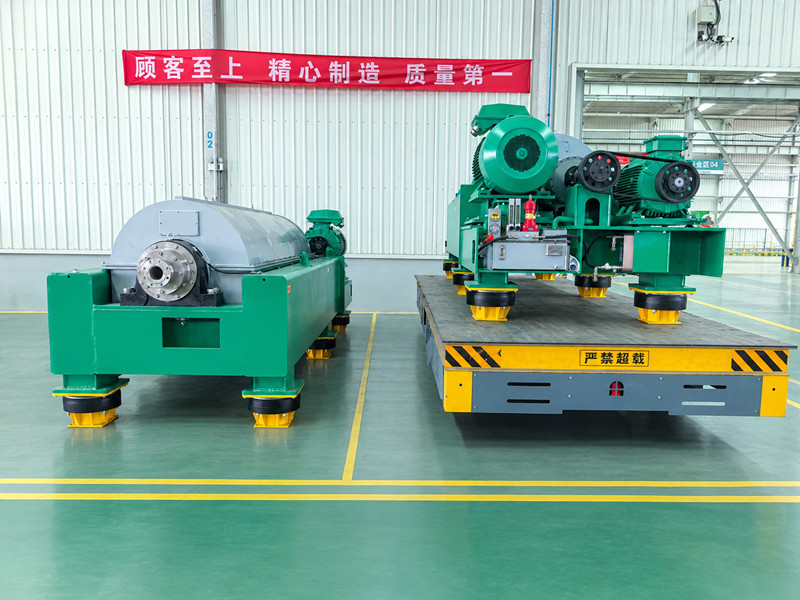
GN Separation’s product range covers decanter centrifuges, sludge dewatering screw presses and complementary separation systems. We partner with clients across mining, wastewater treatment, environmental remediation and a wide array of industrial sectors. Our team keeps innovating field-proven separation technologies to help operators boost process efficiency and overcome solid-liquid separation challenges.
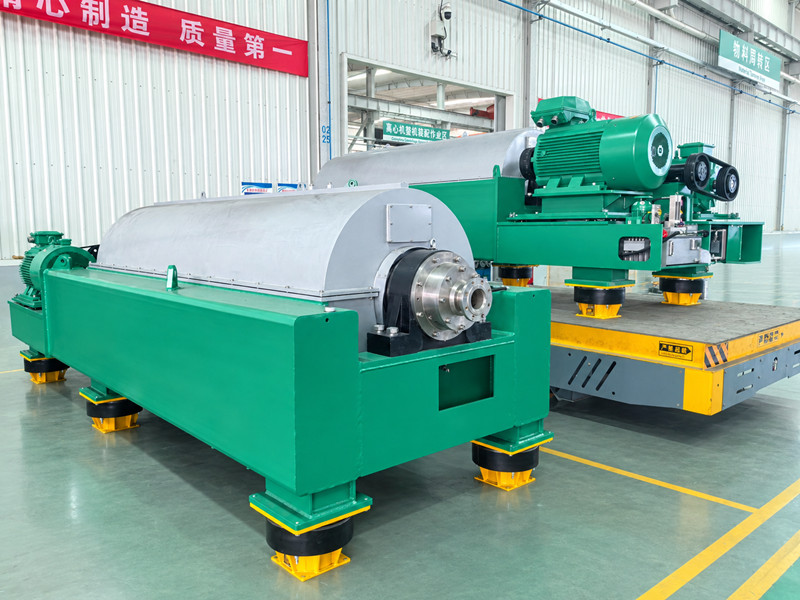
As the GNLW764 Large-Bowl Decanter Centrifuge is set to ship soon, we draw nearer to supporting our client’s mining operation. GN Separation remains committed to delivering trusted separation equipment, advancing efficient solids management and sustainable water recovery for the mining industry.
- Details
-
Published: 25 October 2026