- Details
-
Published: 08 November 2026
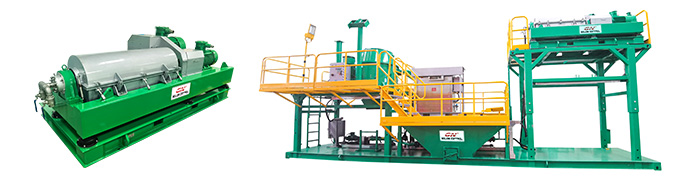
GN Separation delivered a custom‑engineered decanter centrifuge solution for a canola oil clarification project in Australia. Tailored to edible‑oil processing workflows, the unit prioritizes high‑efficiency solid‑liquid separation alongside strict hygiene standards, operational versatility and long‑term operational dependability.
To satisfy the unique demands of edible‑oil production, GN optimized the centrifuge’s internal construction for this Australian end‑user. A core custom modification involves polishing the interior screw conveyor. Fine surface polishing delivers an ultra‑smooth screw surface, lowering material sticking and mitigating build‑up of residual process media within the machine. This feature carries critical importance for food‑grade processing: leftover residues could degrade over time and compromise product sanitary quality. The refined surface also simplifies in‑place cleaning and sustains a hygienic processing environment.
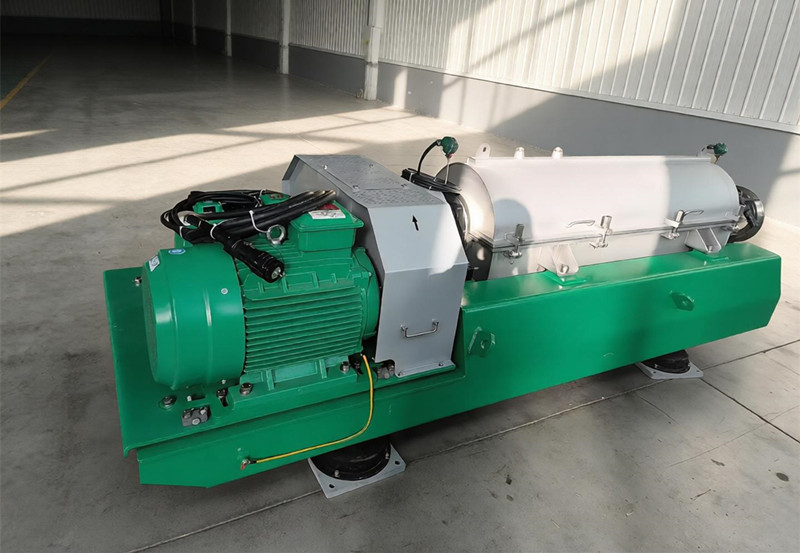
The system is also fitted with a centripetal pump for clarified liquid discharge. Traditional setups frequently require a full shutdown to modify liquid discharge parameters; by contrast, this pump enables operators to adjust the liquid pool depth on‑the‑fly, without halting centrifuge operation. Adjusting the pool depth allows operators to fine‑tune separation performance in response to real‑world feed properties and production targets. Such agility proves highly beneficial when handling feedstock with fluctuating solid loads or shifting process parameters. Unplanned downtime is cut down accordingly, enabling uninterrupted production and boosting overall process efficiency.
Beyond these custom design tweaks, the decanter centrifuge is built for steady, round‑the‑clock operation and consistent separation results. Boasting a compact footprint, continuous solid‑phase discharge and tunable operational parameters, it integrates seamlessly into full‑scale edible‑oil production lines. Equipment specifications are configured to match the client’s process goals, striking an optimal balance between separation efficacy, end‑product quality and ease of operation.
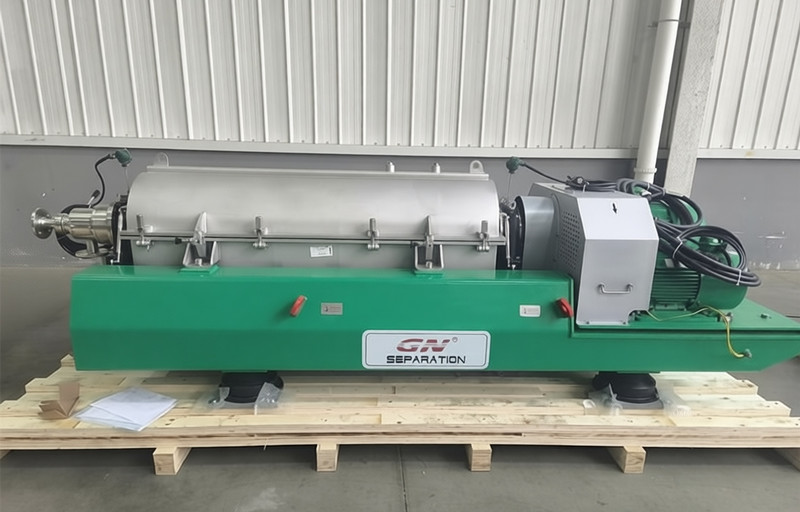
GN Separation possesses profound expertise in designing and fabricating industrial decanter centrifuges serving diverse sectors including food processing, wastewater treatment, oil‑gas and mineral processing. Since feed media and working conditions vary widely from project to project, GN adapts its separation technology to fit each project’s real‑world operational requirements.
This Australian canola‑oil clarification case exemplifies GN’s application‑oriented equipment philosophy. By pairing sanitary internal surface finishing with flexible liquid‑pool depth adjustment, GN supplies the client with a robust separation system that facilitates high‑throughput processing and stable product quality.